Experienced Custom Blending for International Food & Beverage Brands
Greenwood Associates partners with global procurement teams, R&D scientists, and food manufacturers to formulate, blend, and process premium fruit juice concentrates, fruit purees, and complex beverage bases. Backed by over half a century of industry leadership, our technical specialists streamline production, lower cost-in-use, and ensure strict batch-to-batch consistency.
Flexible Batching & Broad Ingredient Integration
Whether you are scaling an existing formula or launching a new functional beverage SKU, our flexible plant capabilities adapt to your exact volume requirements. We handle both small R&D pilot batches and high-volume commercial production runs smoothly.
- Scalable Batch Sizes: Production volumes ranging from 50 to 10,000 gallons per batch.
- Concentrate & Single Strength: Tailored formulation for high-Brix concentrates and single-strength juices.
- Comprehensive Ingredient Matrix: Seamless incorporation of juice concentrates, purees, natural sweeteners, hydrocolloid stabilizers, colors, flavors, vitamins, and minerals.
- Cost Efficiency: Pre-blended master batches reduce raw material inventory complexity at your manufacturing plant.
State-of-the-Art Processing Technology & Bulk Packaging
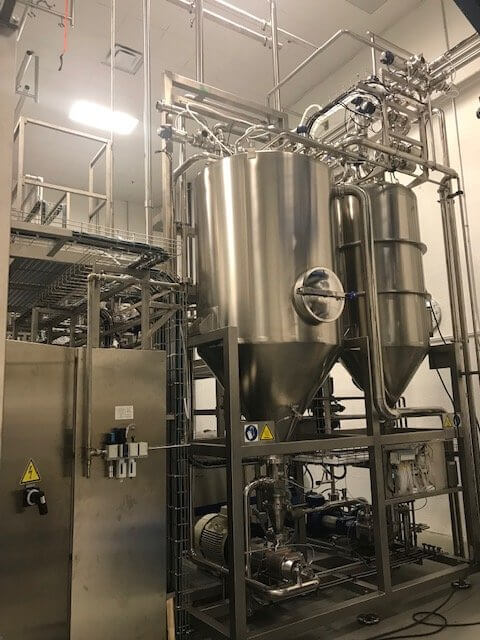
Our U.S.-based processing infrastructure offers versatile thermal treatments and sterile bulk filling formats to maintain product integrity and extend shelf life across international logistics supply chains.
Industrial Processing Options
Our plant operates multiple continuous and batch thermal processing systems designed to preserve natural fruit profile, color, and nutritional value while meeting international food safety standards:
- HTST Pasteurization: High-Temperature Short-Time treatment for pathogen reduction with minimal heat load.
- Batch Pasteurization: Controlled thermal processing for specialized high-viscosity pulp and puree formulas.
- Cold Fill Processing: Cold batching solutions for temperature-sensitive ingredient matrices.
- Aseptic Processing: Sterile filling technology ensuring shelf-stable storage without artificial preservatives.
Industrial Bulk Packaging Formats
We pack finished blends into industry-standard industrial containers built for overseas transit and smooth integration into your filling line:
- 5-Gallon Frozen Pails & 55-Gallon Frozen Drums: Heavy-duty packaging for cold-chain frozen distribution.
- 5-Gallon Aseptic Bag-in-Box (BIB): Convenient ambient-storage format reducing refrigerated freight costs.
- Bulk Totes (275-300 Gallons): High-capacity returnable and non-returnable liquid totes for commercial production lines.
- Bulk Stainless Steel Tankers: Large-scale direct liquid deliveries for high-capacity beverage plants.
Global Food Safety Standards & On-Site Cold Chain
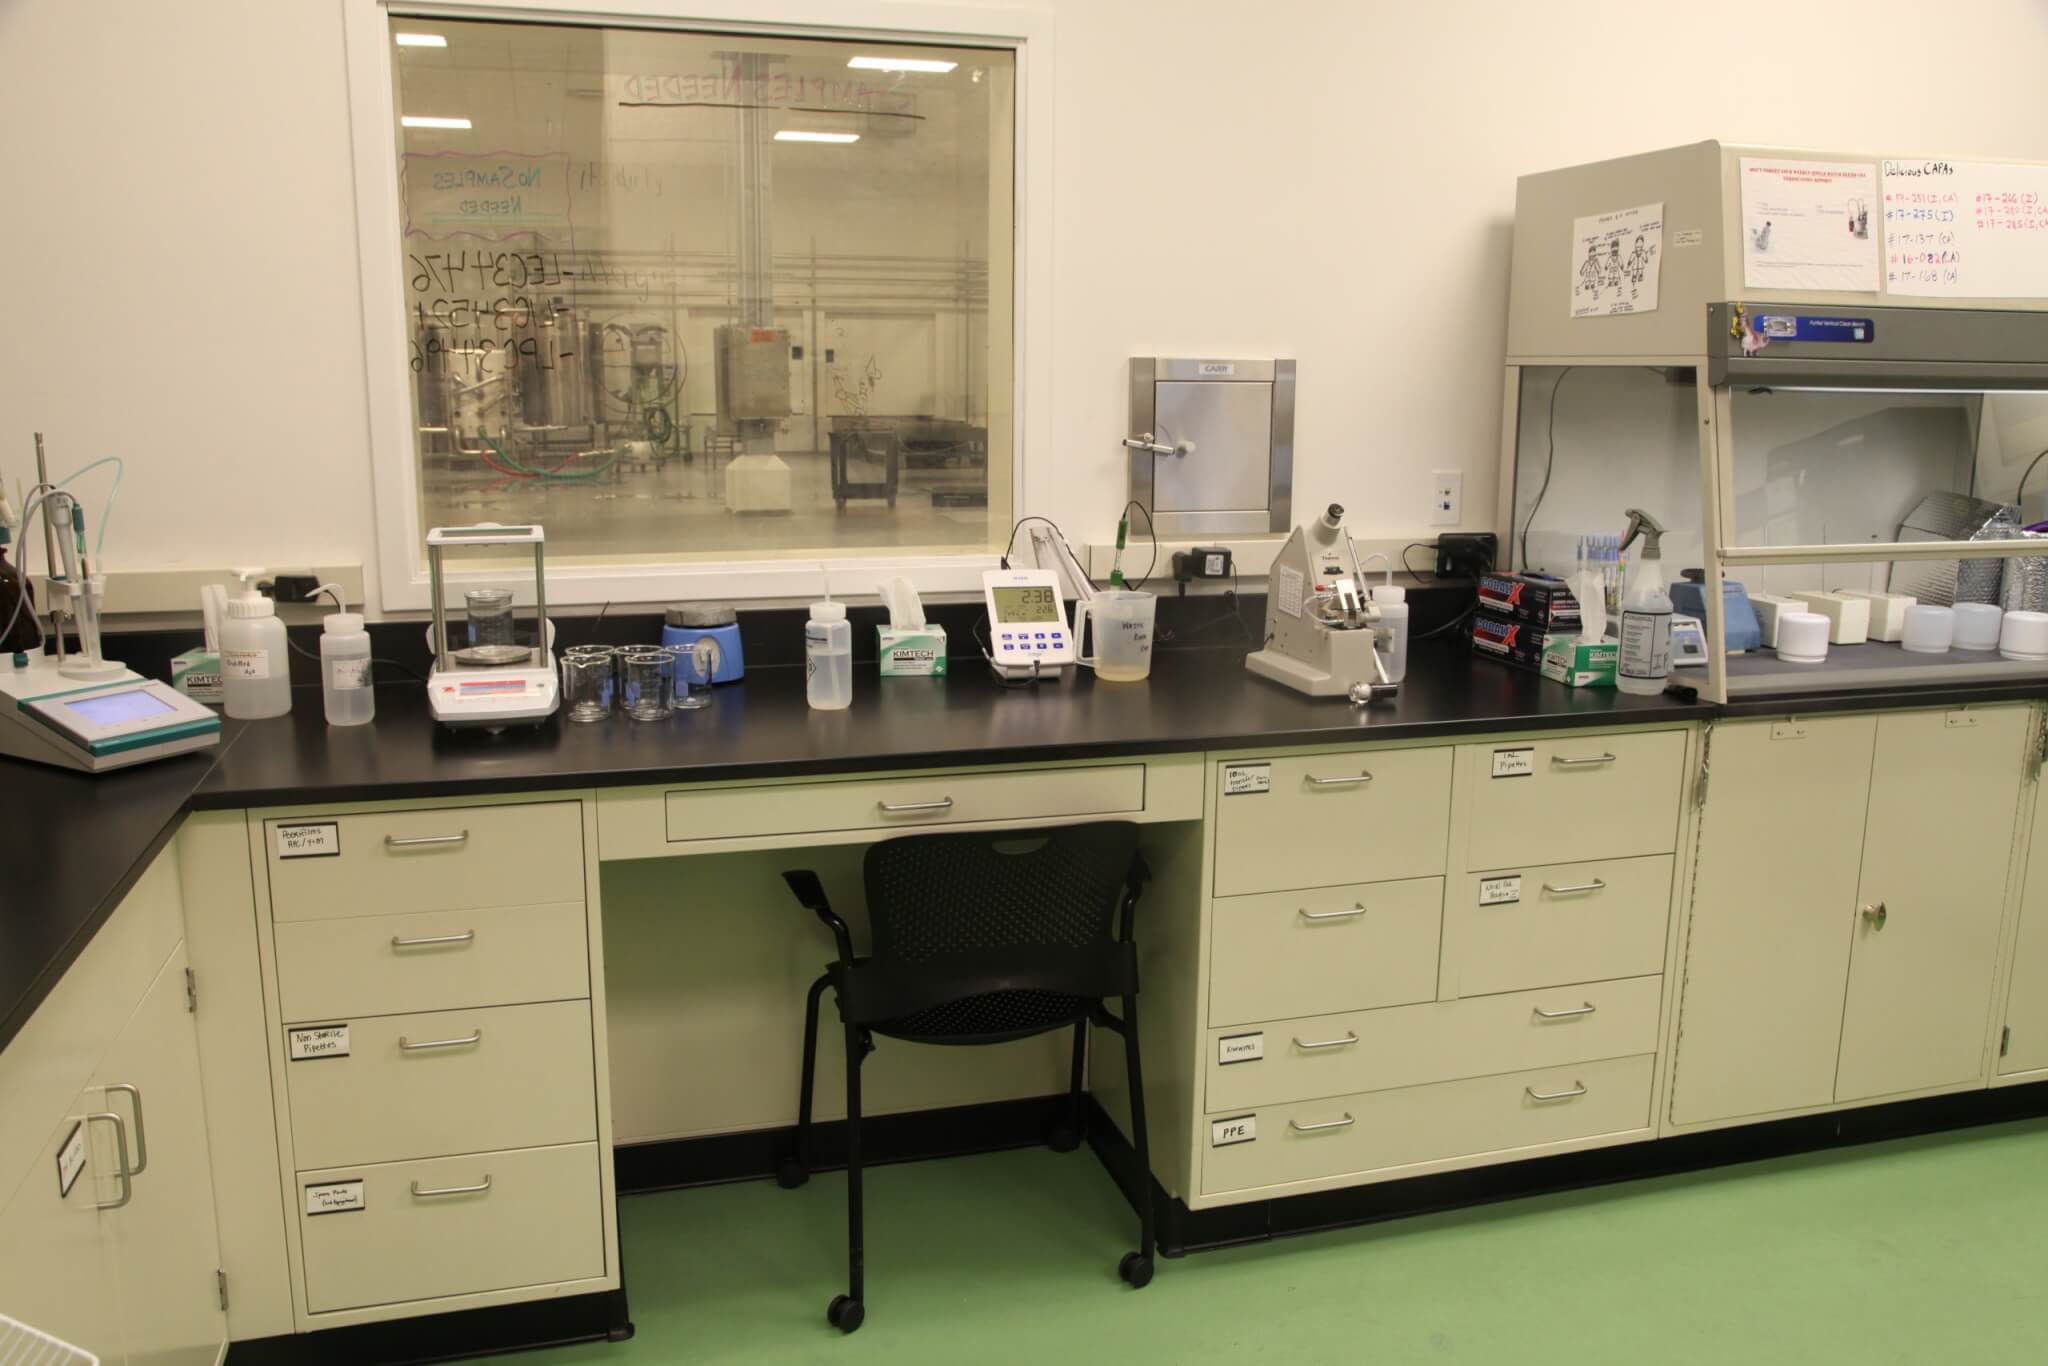
International purchasers trust Greenwood Associates because every custom blend is engineered under stringent Quality Assurance protocols. Our in-house research and analytical laboratory verifies Brix, pH, acidity, sensory parameters, and micro safety for every production lot before dispatch.
- GFSI Certified Facility: Certified under FSSC 22000 for food safety management system excellence.
- Religious & Organic Accreditations: Kosher Certified, Halal Certified (ISA), and USDA Organic certified capabilities.
- In-House Food Safety Lab: HACCP-driven quality control and rigorous batch testing protocols.
- Temperature-Controlled Storage: Multi-zone on-site frozen and refrigerated warehousing ensures product freshness year-round.

Full Traceability & Regulatory Support
We provide complete regulatory support packages for overseas buyers, including Certificates of Analysis (COA), Technical Data Sheets (TDS), Safety Data Sheets (SDS), allergen statements, and country-of-origin documentation.
Discuss Your Custom Blending Project
Connect with our technical business development team to review product specifications, request blend samples, or evaluate contract manufacturing solutions for your market.