Explore our export-grade concentrates, botanical powders, aseptic purees, and specialized plant extracts processed under certified food safety protocols for London beverage manufacturers.
London stands as Europe’s epicenter for commercial beverage innovation. From the high-density premium HORECA sectors of Mayfair and Soho to the craft beverage tech incubators in East London (Shoreditch, Hackney), beverage brand owners face dual commercial imperatives: rigorous consumer demand for clean-label, low-sugar, functional formulations, combined with strict compliance under UK Food Standards Agency (FSA) regulations and the Soft Drinks Industry Levy (SDIL / Sugar Tax).
As a global B2B primary manufacturer and exporter of raw beverage ingredients, custom blended juice bases, citrus essential oils, and functional botanical concentrates, our engineering framework solves complex formulation challenges for London beverage copackers, industrial bottlers, and craft drink brands. Through precise Brix-to-acid ratio adjustments, high-shear homogenisation, natural turbidity control, and thermal preservation, we deliver ready-to-fill and concentrated ingredient bases that perform seamlessly under ambient or cold-chain logistics entering key UK ports such as London Gateway and Tilbury.
Information Gain Insight for Product Developers: Standard commodity juice concentrates often fail in London’s craft RTD market due to excessive natural sugars, variable titratable acidity, or thermal degradation during shipping. Our custom-blended bases utilize ultra-low heat vacuum evaporation and enzymatic stabilization, permitting direct formulation compliance with UK HFSS (High in Fat, Sugar, and Salt) marketing restrictions while preserving native organoleptic profiles.
| Ingredient Base Category | Standard Brix (°Bx) / Concentration | Functional Application Sector | Key Analytical Quality Parameters |
|---|---|---|---|
| Clarified Fruit Juice Concentrates | 65.0° - 70.0° Brix | RTD Sodas, Cider Sweetening, Flavored Waters | NTU Turbidity < 2.0, Zero Pectin Residue, Color Stability |
| Aseptic Single-Strength Purees | 8.0° - 18.0° Brix (Natural) | Craft Smoothies, HORECA Cocktail Bases, Dairy | Cell-wall suspension stability, Zero added sugars, Micro-free |
| Water-Soluble Botanical Powders | Spray-Dried / Freeze-Dried 100% Soluble | Functional Energy Shots, Wellness Teas, Nootropic Mixes | Instant dissolution in cold water, Active Polysaccharide Assay verified |
| Citrus Essential Oils & Terpenes | 100% Pure Cold-Pressed / Folded Oils | Distilled Spirits, Non-Alcoholic Gin Mixers, Flavors | Gas Chromatography (GC-MS) verified terpene fold ratios |
| Custom Blended Beverage Compounds | Engineered per Customer SOP (40°-65° Brix) | Private Label Bottling, Fountain Syrups, RTD Cans | Pre-balanced pH (2.8 - 3.6), Titratable Acidity, Preservative-free |
Bespoke blending of high-intensity fruit juice concentrates with natural acidulants to minimize taxable sugar content while maximizing natural mouthfeel and sweetness perception.
Advanced liquid extract blending featuring non-GMO fungal polysaccharides (Mushroom Concentrates) and adaptogenic plant extracts (Graviola/Soursop) engineered for stable suspension without sediment.
Container solutions ranging from 5-gallon (20L) pails for startup R&D trials in London pilot plants, up to 200L aseptic drums and 1000L totes for full-scale contract bottling lines.
Commercial success in London’s dynamic beverage market requires ingredients that cater directly to hyper-localized consumer preferences. Our export operations specifically support five high-growth market segments across the UK capital:
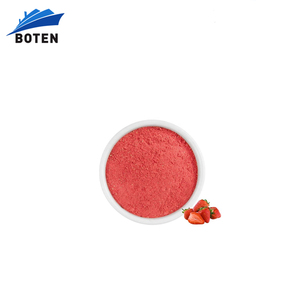
London leads global trends in the "Mindful Drinking" movement. Upscale venues across Soho, Covent Garden, and the City require sophisticated, non-alcoholic bases that replicate the viscosity, tartness, and aromatic complexity of traditional spirits. Utilizing our Water Soluble Strawberry Juice Concentrate Powders, Clarified Cranberry Juice Concentrates, and Citrus Essential Oil Fractions, London flavor houses create complex aperitifs, alcohol-free gin alternatives, and low-ABV cocktail syrups. Our pasteurization protocols preserve volatile aromatic esters, eliminating cooked off-flavors typical of lower-grade industrial concentrates.
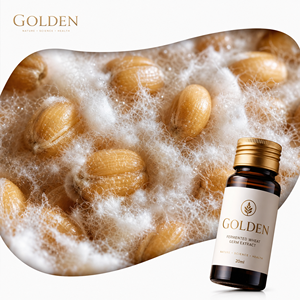
The health-conscious commuter demographic in financial hubs such as Canary Wharf and Bank has fueled massive demand for 60ml functional wellness shots. Formulating these products requires high ingredient solubility and active bio-component standardization. Our Mushroom Extract Liquid Concentrate (Polysaccharide Standardized) and Graviola (Soursop) Plant Extracts provide clean functional claims without sacrificing taste clarity or causing cloud sedimentation in flash-pasteurized shelf-stable shots.
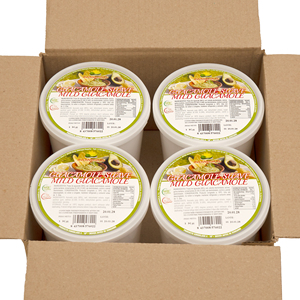
London's premium food service sector demands stable fruit ingredients capable of surviving high-heat processing while retaining vibrant visual appeal. Products such as our Artisanal 1kg Frozen Smooth Guacamole Tubs and Sterilized Frozen Strawberry Purees allow commercial kitchens, high-end bakery chains, and foodservice distributors across Greater London to maintain absolute batch consistency without synthetic preservatives or artificial colorants.
Contract packers operating in Essex, Kent, and the Home Counties supplying London supermarket chains require bulk juice concentrates delivered in 1000L aseptic totes. By standardizing Brix levels and titratable acidity across multi-ton shipments, we eliminate the need for line operators to adjust dilution formulas between production batches, reducing plant downtime and operational yield loss.
Procuring raw beverage ingredients internationally requires precise communication between your internal R&D chemists, quality assurance (QA) managers, and commercial procurement buyers. To streamline technical evaluation and sample matching, we recommend establishing clear parameters across four key vectors:
Specify whether your product requires single-strength juice (NFC), high-ratio concentrate (e.g., 65° Brix), or pureed pulp. For RTD carbonated soft drinks, clarified concentrates prevent nozzle clogging during high-speed filling. For smoothies or fruit-based beers, unclarified purees provide desired cloud density and mouthfeel.
Select packaging compatible with your plant’s receiving infrastructure. Aseptic Bag-in-Box (10L / 20L) and Aseptic Totes (1000L) allow ambient storage prior to opening, drastically reducing expensive frozen cold-storage electricity costs in London industrial parks where commercial energy rates remain high.
Confirm whether your final product will claim "No Added Sugar," "100% Natural Origin," "Organic (UK Cert)," Kosher, or Halal. Providing these requirements upfront allows our quality control laboratory to supply compliant certificates of analysis (CoA) alongside sample batches.
Utilize our low MOQ pail program (5-gallon / 20kg) to run benchtop pilot trials and initial shelf-life stress testing. Once formula stability is confirmed, seamlessly transition to drum or tote production orders under identical processing SOPs.
Technical and logistical answers to common questions asked by UK food & beverage purchasing teams.
We provide one of the most flexible ordering structures in the primary ingredient manufacturing sector. For standard stocked fruit juice concentrates, botanical powders, and aseptic purees, our MOQ starts as low as a single 5-gallon (20L) pail or one bag-in-box unit. For custom proprietary blends formulated to your specific Brix and pH parameters, minimum run sizes depend on formula complexity but typically start at 1 drum (200L) for pilot testing, scaling easily to full 20ft container loads for commercial bottling runs.
The UK Soft Drinks Industry Levy (SDIL) applies to added-sugar drinks containing 5g or more sugar per 100ml. Our food technologists design low-glycemic fruit compound bases by blending naturally sweet, high-acid fruit concentrates with water-soluble botanical extracts and natural flavor enhancers. This allows London bottlers to achieve optimal flavor impact and mouthfeel while keeping total sugar levels below the lower tax threshold tier.
All ingredient manufacturing, blending, and aseptic packing facilities operate under the stringent FSSC 22000 (Food Safety System Certification) framework, audited by third-party Registrar standards. Furthermore, we maintain full Kosher certification and Halal certification issued by Islamic Services of America (ISA). Full Certificate of Analysis (CoA), Allergen Statements, Non-GMO Declarations, and Heavy Metal test results are provided with every batch lot shipped into the UK.
For operations with limited cold-storage capabilities, we recommend our Aseptic Bag-in-Box (20L) or Aseptic Steel Drums (200L). These products undergo ultra-high temperature (UHT) flash sterilisation followed by sterile filling into oxygen-barrier barrier bags. They maintain ambient shelf life for up to 12-18 months unopened, allowing convenient warehouse storage until opened for tank mixing.
Yes. Our state-of-the-art co-packing facility accepts bulk raw materials, intermediate totes, or single-strength juices, and processes them to customer specification. We offer custom blending, filtration, pasteurization, and re-packing into customer-branded pails, aseptic bags, drums, or totes complete with custom product labeling, batch numbering, and barcode traceability.
Stocked catalog items dispatch from our main warehousing hubs within 48-72 hours. Sea freight shipping to London Gateway or Tilbury typically takes 10 to 14 days, followed by customs clearance and local door-to-door freight delivery directly to your plant. For urgent pilot trials or R&D launches, expedited air freight delivery for pails and sample kits can be arranged within 3-5 business days.
Whether you are reformulating an existing beverage line to meet UK clean-label guidelines or scaling up a novel functional RTD concept in London, our technical team is ready to assist with samples, custom compounding, and dedicated export supply.