Explore our ready-to-ship aseptic fruit concentrates, functional extracts, and standardized vegetable purees for commercial formulation.
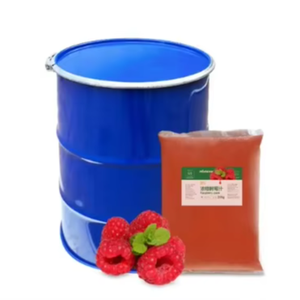
New Zealand's dynamic food and beverage industry—ranging from craft cideries in Hawke's Bay to dairy fortification facilities in the Waikato and functional beverage innovators in Auckland—demands uncompromising quality, absolute biosecurity compliance, and cost-effective bulk ingredient sourcing.
Every shipment of fruit concentrate and puree exported from our Chinese processing facility undergoes strict thermal validation. We supply comprehensive documentation ensuring smooth clearance via the New Zealand Ministry for Primary Industries (MPI).
Our Bag-in-Box (BIB) technology utilizes high-barrier multi-layer aluminum EVOH films, locking in organoleptic qualities, fresh aromas, and naturally vibrant colors without artificial preservatives or cold-chain dependence during ambient ocean transit.
We tailor Brix levels, pH ratios, and clarity parameters (clarified vs. cloudy) to match precise beverage base recipes. Our in-house research laboratory ensures lot-to-lot consistency for seamless line blending.
For New Zealand beverage manufacturers and food processors, freight efficiency, container utilization, and product integrity are critical metrics. Traditional frozen juice drums require energy-intensive refrigerated containers (reefers) and thawing infrastructure. Our China factory's high-tech Aseptic Bag-in-Box solutions solve these supply chain bottlenecks.
| Specification Parameter | Factory Benchmark Standard |
|---|---|
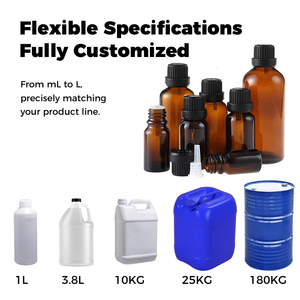
| Packaging Sizes | 10L, 20L Bag-in-Box (Carton) / 200L Aseptic Drum |
| Sterilization Process | High-Temperature Short-Time (HTST) / UHT Flash Sterilization |
| Oxygen Barrier (OTR) | < 0.1 to 0.5 cm³/m²·24h·0.1MPa (ISO 15105-2) |
| Microbiological Standard | Commercially Sterile (TPC < 10 CFU/g, Yeast & Mold < 10 CFU/g) |
| Storage Condition | Ambient Storage (< 25°C recommended), Cool storage for citrus |
| Quality Certifications | FSSC 22000, ISO 22000, Kosher, Halal (ISA Certified), HACCP |
| Export Ports | Qingdao, Ningbo, Shanghai to Auckland, Tauranga, Lyttelton |
From large-scale commercial bottling plants in South Auckland to artisanal boutique producers in the South Island, our fruit concentrates and extract powders elevate product formulations across key sectors.
New Zealand's craft brewing and cider industry relies on our high-clarity Raspberry, Strawberry, and Pineapple Concentrates for secondary fermentation, fruit beers, RTD beverages, and flavored seltzers requiring high Brix and consistent acid profile.
Export-grade NZ yogurts, flavored milks, and artisanal ice creams utilize our standardized fruit purees and water-soluble powders for vibrant taste, zero artificial color addition, and smooth texture integration.
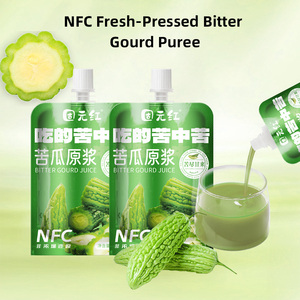
Capitalize on the growing wellness market with active functional ingredients like High Purity Phyllanthin Powder, Mushroom Liquid Concentrates, and bitter melon purees designed for immune-support shots and nutraceutical beverages.
As a leading Chinese wholesale manufacturer with decades of processing expertise, we bridge the gap between agricultural abundance and industrial food science. Our integrated facilities handle every production stage—from farm-level raw material selection to automated extraction, concentration, and aseptic packaging.
Quality assurance is embedded in our operational DNA. Every batch of fruit concentrate undergoes comprehensive analytical testing prior to dispatch:
Official certificate copies and Certificate of Analysis (COA) supplied with every sample and shipment.
Essential insights for procurement managers, food technologists, and supply chain directors importing bulk fruit concentrates from China to New Zealand.
We provide flexible MOQ parameters tailored to your business scale. For R&D trials, pilot batches, or commercial recipe development, orders can start as low as a single 20L Bag-in-Box or 5-gallon pail. For commercial production runs, we recommend pallet quantities (approx. 44 to 60 boxes) or 20ft Full Container Loads (FCL) to achieve optimal ocean freight cost efficiency to Port of Auckland or Tauranga.
Our aseptic manufacturing process includes validated thermal processing (HTST/UHT) that satisfies biosecurity requirements for plant-derived fruit juices and purees. Every shipment includes a official Phytosanitary Certificate (when required), Manufacturer Declaration, Certificate of Analysis (COA), and complete bill of lading documentation to facilitate fast border clearance with NZ Customs and MPI inspectors.
Direct ocean freight service from major Chinese departure ports (Qingdao, Ningbo, Shanghai) to New Zealand ports (Auckland, Tauranga, Lyttelton/Christchurch) typically takes between 14 to 18 days depending on the shipping line. Including customs clearance and local dispatch, total lead time from order confirmation to plant arrival is usually within 25 to 30 days.
Yes. Our in-house research laboratory specializes in custom product development. We can blend multiple juice concentrates, standardize Brix levels (e.g., 65° Brix Apple or Grape bases), adjust acidity levels, or co-pack proprietary formulation bases delivered directly in sterile Bag-in-Box packaging ready for your production line.
Because our Bag-in-Box products are commercially sterile, unopened packages can be stored under ambient warehouse conditions (< 20°C to 25°C) away from direct sunlight. For prolonged shelf life beyond 12 months or for sensitive citrus products (such as orange or lemon concentrates), cool storage at 4°C to 8°C is recommended to preserve peak color and fresh flavor notes.
Every commercial shipment comes standard with a comprehensive documentation package: Batch-Specific Certificate of Analysis (COA), Commercial Invoice, Packing List, Bill of Lading, FSSC 22000 / ISO Quality Certificates, Halal/Kosher Certificates, and Non-GMO / Allergen Declarations.
Request pricing, factory specification sheets, or commercial samples for your product development team. Our international export team responds within 12 business hours.