Engineered for HORECA distributors, commercial bakeries, dairy processors, and beverage manufacturers. Our aseptic and IQF frozen fruit solutions preserve 100% natural Brix integrity and volatile aroma compounds without artificial additives.
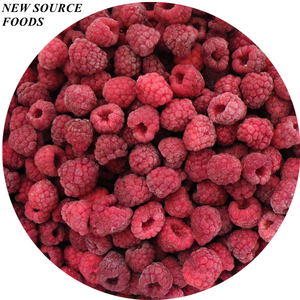
Premium Grade-A whole raspberries, individually quick-frozen at harvest peak to maintain structure, vibrant color, and sweet-tart flavor profile for bakery & puree processing.
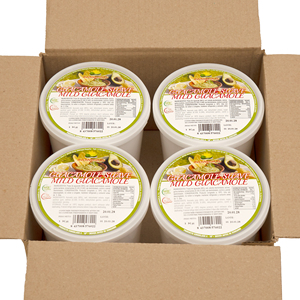
High-pressure processed (HPP) smooth avocado guacamole tub. Designed for commercial food service & hospitality clients demanding consistent rheology and long shelf life.
100% natural Hass avocado pulp packed in food-grade pails. Zero anti-browning chemicals, maintaining rich lipid texture and authentic natural mouthfeel.
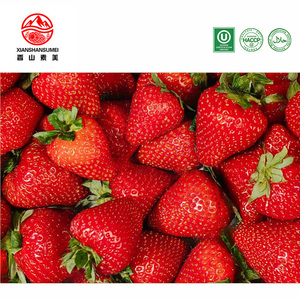
Factory-direct bulk strawberry supply. Calibrated sizing with controlled Brix ratio, ideal for industrial jam production, confectionery, and dairy fruit preps.
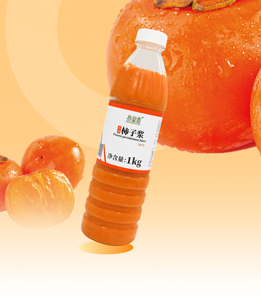
Exotic tropical fruit puree harvested from sweet non-astringent persimmons. Flash pasteurized and aseptic/frozen filled for beverage formulation & craft brewing.
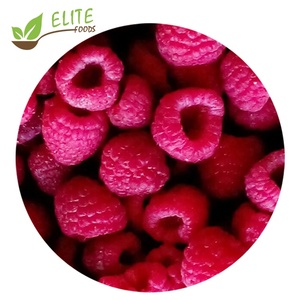
Strictly audited industrial raspberries with guaranteed 80%+ fruit intactness. Exceeds global micro-specifications for high-end retail packaging and dessert production.
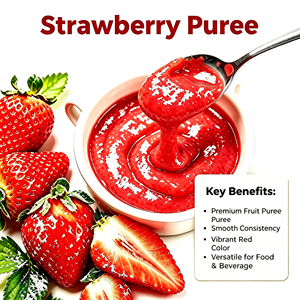
OEM/ODM pureed strawberry concentrate without added sugar or colorants. Ultra-clean microbial profile verified by in-house laboratory testing for global distribution.
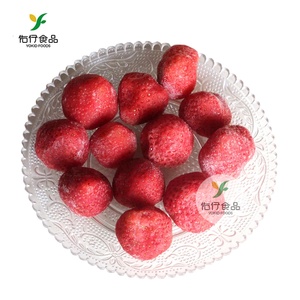
Coarse-ground strawberry mash formulated specifically for paste manufacturing, fruit filling bases, and commercial topping prep lines. High seed retention option available.
How non-thermal preservation, clean-label formulation, and rheological engineering are reshaping commercial fruit processing.
The global food and beverage industry is experiencing a profound paradigm shift. Industrial procurement managers, R&D food scientists, and master blenders are moving beyond conventional thermal-heavy purees toward advanced clean-label, minimally processed fruit solutions. As consumer demand for authentic organoleptic profiles, natural colors, and uncompromised nutritional integrity reaches an all-time high, fruit puree manufacturers must integrate state-of-the-art processing methodologies.
Traditional fruit concentration methods often relied on high-temperature, long-time pasteurization. While effective for thermal destruction of vegetative pathogens, this legacy process degraded delicate ester fractions, oxidized natural polyphenols, and caramelized naturally occurring sugars—resulting in altered color and a burnt flavor note.
Leading manufacturers now utilize short-time flash pasteurization combined with Aseptic Cold Filling and High-Pressure Processing (HPP). By subjecting purees to hydraulic pressures up to 600 MPa (87,000 psi) or employing rapid aseptic thermal loops, microbial vegetative cells are inactivated while preserving aromatic volatiles (such as hexanal in berries and linalool in citrus). This allows R&D teams to formulate final products with a fresh fruit taste profile without adding artificial flavor enhancers.
Modern high-speed automated bottling and dosing lines demand exact physical performance parameters. A puree that varies in viscosity from batch to batch causes dosing inaccuracies, nozzle clogging, and line downtime. Today's commercial purees undergo rigorous rheological profiling, measuring parameters such as:
Regulatory bodies and consumers worldwide are scrutinizing added sugars, synthetic antioxidants, and chemical preservatives like sodium benzoate or potassium sorbate. The modern industrial standard mandates single-ingredient fruit purees or purees stabilized solely with natural ascorbic acid (Vitamin C) for browning prevention.
| Processing Parameter | Legacy Hot-Fill Puree | Modern Aseptic Frozen Puree | High-Pressure Processed (HPP) Puree |
|---|---|---|---|
| Thermal Exposure | High (85°C – 95°C for 2–5 mins) | Ultra-Short Flash (90°C for 15–30 secs) | Non-Thermal (Ambient / Chilled) |
| Aroma & Volatile Retention | Moderate degradation (Caramelization) | High (90%+ Volatile Retention) | Exceptional (Near 100% Fresh Profile) |
| Enzyme Inactivation (PPO) | Complete | Complete | Targeted Inactivation |
| Shelf Life & Storage | Ambient / Refrigerated | Ambient Aseptic (12-18 Mos) / Frozen (-18°C) | Refrigerated Cold-Chain (60-90 Days) |
| Primary Industrial Application | Low-cost mass bakery filling | Beverage, Dairy, Craft Brewing, HORECA | Ultra-Premium Clean Label, Functional Juices |
Navigating climate volatility, freight inflation, dual-hemisphere sourcing, and stringent food safety documentation.
To mitigate crop loss from extreme weather events, tier-1 procurement directors are moving away from single-origin dependency. Partnering with suppliers with orchards across both Northern and Southern hemispheres guarantees year-round harvest coverage and price stability.
With reefer container freight rates subject to volatility, manufacturers are increasingly specifying Aseptic Bag-in-Box (BIB) and Aseptic 200L Drums. Ambient aseptic storage drastically lowers energy footprints and ocean freight tariffs while maintaining sterile integrity.
Food fraud and fruit juice adulteration (e.g., diluting costly passion fruit or raspberry with apple juice concentrate) are fought via SNIF-NMR (Site-Specific Natural Isotope Fractionation) and isotopic testing, accompanied by lot-specific digital Certificates of Analysis (COA).
In an era of economic fluctuation, fixed spot-market purchasing exposes food manufacturers to severe margin compression. Industrial buyers are shifting toward multi-quarter volume reservations anchored by Brix-indexed contract pricing. By securing crop commitments during early harvest windows, manufacturers buffer their supply chains against supply shocks, currency devaluation, and sudden tariff adjustments.
For over half a century, our family-owned enterprise has delivered uncompromised quality control, flexible industrial packaging, and tailored custom blending solutions.
Our processing facilities operate under rigorous global benchmarks: FSSC 22000 Food Safety System Certification, Kosher Certification, and ISA Halal Certification. Every production run is audited in our internal microbiology & wet chemistry lab.
From pilot R&D trials to full commercial runs, we support all production scales. Order as little as a single 5-gallon pail or 20kg Bag-in-Box, up to 200L aseptic steel drums and 1000L returnable IBC totes.
Need a specific Brix-to-acid balance or proprietary multi-fruit signature blend? Our R&D team reformulates ingredients to your exact line specifications, offering contract co-packing and private labeling.
Headquartered in Niles, Illinois, Greenwood Associates operates an integrated warehousing network strategically positioned across primary transportation corridors to minimize freight transit times and preserve cold-chain integrity:
Essential technical and commercial information for Quality Assurance, R&D, and Purchasing teams.
Greenwood Associates offers one of the most flexible MOQ structures in the commercial fruit industry. Purchasing units start as low as a single 5-gallon pail or 20kg aseptic bag-in-box (BIB) for R&D pilot plant trials and niche production runs. Full pallet, 200L drum, and 1000L tote shipments are available for full-scale commercial manufacturing.
IQF (Individually Quick Frozen) Fruit consists of 100% whole or diced fruit frozen rapidly to maintain physical cellular integrity (-18°C), ideal for bakery toppings, IQF retail packs, and whole-fruit preps. Aseptic Puree is flash-sterilized and packed into sterile barrier bags, allowing ambient shipping and storage prior to opening. Cold-Filled Frozen Puree is pureed and frozen immediately without ambient shelf stability, maximizing raw volatile aroma preservation.
Agricultural crops naturally fluctuate in sugar (°Brix) and titratable acidity (TA) due to weather patterns. Our state-of-the-art laboratory analyzes every harvest batch. Through master blending techniques, we standardize °Brix-to-acid ratios within tight spec tolerances (+/- 0.5° Brix) to ensure your automated production line receives identical ingredient inputs year-round.
We supply full documentation packages for QA compliance. Every lot includes a Certificate of Analysis (COA) detailing Brix, pH, Titratable Acidity, Bostwick viscosity, Total Plate Count (TPC), Yeast & Mold counts, and E. coli / Salmonella screens. Facilities are certified under FSSC 22000, BRCGS Grade-A, Kosher, and ISA Halal.
To preserve color and flavor while preventing microbial growth, frozen purees should be thawed in controlled refrigerated rooms at 2°C – 4°C (35°F – 40°F) over 48 to 72 hours with periodic agitation if packed in drums. Avoid high-temperature water baths or ambient room exposure exceeding 20°C to prevent enzymatic oxidation and quality degradation.
Yes. Our product development team specializes in custom co-packing and formulating proprietary fruit bases. We can adjust fiber levels, seed counts, blend complementary superfruits (e.g., strawberry-raspberry or persimmon-citrus), and incorporate natural antioxidants or sweeteners to meet your exact label target.
Partner with a trusted U.S. manufacturer with over 50 years of processing heritage. Request lab samples, customized spec sheets, or volume price quotations today.