Discover our ready-to-ship aseptic fruit concentrates, processed vegetable purees, and clean-label extracts tailored for commercial food, beverage, and nutraceutical processing.
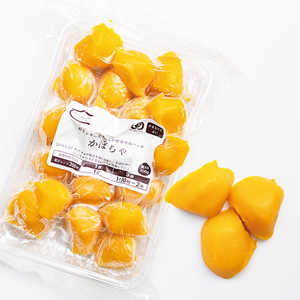
Sweet potato puree has evolved from a traditional agricultural commodity into a critical functional ingredient across commercial food manufacture, pet nutrition, baby food, and clean-label beverage formulation. Driven by consumer demand for naturally sweet, nutrient-dense, and unrefined carbohydrate sources, procurement managers must navigate complex rheological, thermal, and microbiological variables when selecting a global supplier.
Sweet potato puree retains exceptionally high levels of beta-carotene (provitamin A), dietary fiber, potassium, and complex starches. Orange-fleshed varieties (Covington, Beauregard) yield vibrant natural color and high natural Brix, reducing added sugar requirements in end formulations.
Starch gelatinization during steam cooking imparts specific pseudoplastic flow properties. High-shear enzyme-treated purees deliver low Bostwick consistency values suited for ready-to-drink beverages, while single-strength aseptic purees maintain rich body for bakery fillings.
Serves as a functional binder, moisture retainer, and natural colorant. It replaces synthetic gums, high-fructose corn syrup, and modified starches in consumer packaged goods (CPG), fulfilling non-GMO and organic clean-label mandates.
Procurement teams should evaluate prospective suppliers against standardized physical, chemical, and microbiological parameters to guarantee plant-level consistency:
| Parameter Grade | Single-Strength NFC Puree | De-starched / Enzymatic Puree | Concentrated Sweet Potato Puree | Testing Method / Standard |
|---|---|---|---|---|
| Brix Level (°Bx) | 14.0° – 18.0° Brix | 18.0° – 24.0° Brix | 28.0° – 32.0° Brix | Refractometer @ 20°C |
| pH Spectrum | 5.2 – 6.0 | 5.0 – 5.8 | 4.8 – 5.6 | pH Meter Direct Measurement |
| Bostwick Viscosity | 3.0 – 7.0 cm / 30 sec (@20°C) | 12.0 – 18.0 cm / 30 sec | 1.0 – 4.0 cm / 30 sec | Bostwick Consistometer |
| Processing Method | Steam Blanched & Pureed | Enzymatic Hydrolysis | Vacuum Evaporation | Thermal Process Validation |
| Microbial Standard | Commercial Sterility | Commercial Sterility | Commercially Sterile / Frozen | TPC < 10 CFU/g (Aseptic) |
| Certifications | FSSC 22000 / Kosher / Halal | FSSC 22000 / Kosher / Halal | FSSC 22000 / Kosher / Halal | Third-Party Audit Certificates |
Our SEO research and food engineering teams have conducted an extensive benchmarking analysis of leading global bulk B2B suppliers based on manufacturing capacity, quality compliance (GFSI), custom formulation flexibility, minimum order quantities (MOQ), and supply chain reliability.
Headquarters: Niles, Illinois, USA | Experience: 50+ Years Family-Owned
Core Capabilities: Greenwood Associates stands out as an industry leader for custom blending, aseptic packaging, and low-MOQ supply of fruit and vegetable concentrates and purees. With over half a century of family ownership, Greenwood operates an advanced in-house quality testing laboratory, running strict HACCP protocols to inspect every lot before shipment.
Supply Chain Advantage: Maintaining one of the lowest minimum order quantities in North America (available in quantities as small as a single 5-gallon pail or bag-in-box up to totes and drums), Greenwood operates an expansive U.S. warehouse network across Illinois, California, Texas, Florida, Ohio, Minnesota, Georgia, New Jersey, Nevada, and Massachusetts.
Certifications: FSSC 22000, Kosher Certified, Halal Certified (Islamic Services of America - ISA).
Headquarters: Darmstadt, Germany | Global Reach: 160+ Countries
Overview: Döhler is a global technology-driven producer of natural ingredients, fruit juices, and vegetable purees. Their sweet potato puree lines emphasize enzymatic liquefaction for seamless integration into beverage formulations and smoothie bases without gritty mouthfeel.
Key Strengths: Integrated ingredient systems, global flavor development capabilities, and extensive industrial contract manufacturing.
Headquarters: Vienna, Austria | Specialty: Agricultural Processing
Overview: AGRANA specializes in high-value fruit preparations and industrial starch/vegetable processing. Their sweet potato ingredients target dairy processors, providing fruit-and-vegetable preparations for yogurts, puddings, and infant nutrition.
Key Strengths: Strong European agricultural sourcing network, robust traceability, and non-GMO organic crop contracts.
Headquarters: Breda, Netherlands | Specialty: Fruit & Vegetable Ingredients
Overview: Backed by agrarian cooperatives, SVZ supplies premium single-strength and concentrated sweet potato purees to CPG manufacturers across Europe and the Americas. Their low-heat sterilization techniques preserve natural carotene colors.
Key Strengths: Sustainable agronomy programs, high-yield aseptic processing, and low heavy-metal risk mitigation for infant food.
Headquarters: Selah, Washington, USA | Specialty: Fruit & Puree Co-op
Overview: Widely recognized for apple and fruit products, Tree Top’s ingredient division processes high-grade North American sweet potatoes into smooth, heat-stable purees used extensively in bakery products, pet food treats, and CPG sauces.
Key Strengths: US grower cooperative ownership, stringent pesticide testing, and large-scale industrial drumming options.
Headquarters: Salem, Oregon, USA | Specialty: Custom Juice & Puree Concentrates
Overview: Operating under Ingredion, Kerr Concentrates crafts high-brix sweet potato purees and custom blends. They specialize in tailoring color, sweetness, and solids levels to fit tight product developer specifications.
Key Strengths: Access to global R&D application centers, custom sensory matching, and starch texture science.
Headquarters: Prosser, Washington, USA | Specialty: Industrial Fruit & Vegetable Purees
Overview: Milne is a trusted industrial processor offering 100% natural sweet potato purees, micro-dried ingredients, and concentrated juices. Their purees are free from artificial additives, preservatives, or added sugars.
Key Strengths: Micro-drying options, continuous pasteurization technology, and strict QA auditing.
Headquarters: Eden Prairie, Minnesota, USA | Specialty: Plant-Based & Organic Ingredients
Overview: SunOpta focuses on organic and non-GMO plant-based food products. Their sweet potato purees serve as key building blocks for plant-based milks, soup bases, and functional CPG formulations.
Key Strengths: Leadership in organic certification, extensive contract packaging, and sustainable sourcing.
Headquarters: Mie, Japan / SE Asia Processing Facilities | Specialty: Purple & Japanese Sweet Potato
Overview: Specialized in unique cultivar processing, Yamamori supplies high-anthocyanin Japanese Purple Sweet Potato (*Ayamurasaki*) and Yellow Sweet Potato purees for premium confectionery and functional beverage applications.
Key Strengths: High anthocyanin pigment retention, exotic variety specialization, and Asian market compliance.
Headquarters: Abbotsford, British Columbia, Canada | Specialty: Pacific Northwest Processing
Overview: Processing high-quality local and imported crops, Pacific Coast Fruit Products offers aseptic bag-in-box and frozen sweet potato purees designed for industrial bakeries, micro-breweries, and regional food brands.
Key Strengths: Flexible regional logistics, batch-level quality control, and custom drum packing.
Procurement leadership must look beyond unit price and align with strategic technological innovations and agricultural shifts impacting the bulk puree ecosystem through 2030.
Advanced alpha-amylase and glucoamylase enzymatic processing allows suppliers to break down insoluble starches into soluble maltodextrins without adding artificial sugars. This enables high-Brix liquid sweet potato purees that flow smoothly in automated pumps and beverage pasteurizers.
Transitioning from energy-intensive frozen drums to ambient-stable aseptic Bag-in-Box (BIB) and Totes drastically reduces cold-chain freight expenditures and storage carbon footprints while extending un-opened shelf life to 12–18 months.
Sustainability mandates are pushing food giants toward "upcycled certified" sweet potatoes—utilizing misshapen or aesthetically imperfect tubers that possess identical nutritional profiles, reducing field-level food waste while optimizing raw material costs.
Why Global Procurement Managers Rely on Greenwood for Custom Purees, Concentrates, and Blends
For more than 50 years, family-owned Greenwood Associates (headquartered in Niles, IL) has provided end-to-end supply stability for fruit and vegetable ingredients. Unlike rigid industrial brokers, Greenwood delivers flexible, high-value services designed to remove procurement friction:
Follow this 4-step framework to qualify suppliers and guarantee seamless plant execution:
Specify target Brix (14°–30°), Bostwick viscosity range, and mesh fineness (e.g., 0.033" vs 0.060" screen size).
Request current audit certificates for GFSI (FSSC 22000/SQF), Kosher, Halal, Allergen-free, and Non-GMO statements.
Determine handling requirements: 5-gallon pails for pilot batches, 55-gallon aseptic drums, or 2200 lb liquid totes.
Evaluate benchtop samples for color retention, enzymatic stability, retrogradation resistance, and flavor fidelity.
Expert insights addressing critical technical and commercial procurement inquiries.
Single-strength (Not-From-Concentrate / NFC) sweet potato puree is produced by washing, peeling, steam-blanching, and pureeing whole roots without water removal, typically yielding 14° to 18° Brix. Concentrated sweet potato puree undergoes thermal vacuum evaporation to remove water content, reaching 28° to 32° Brix. Concentrates significantly reduce freight costs per pound of solids but require reconstitution equipment in your plant.
While many global processors require full truckload (FTL) or multi-drum commitments, specialized suppliers like Greenwood Associates offer industry-leading flexible MOQs. Products can be ordered in quantities as small as a single 5-gallon pail or one aseptic bag-in-box, ideal for pilot scale operations, R&D formulation trials, or craft production runs.
For commercial distribution, suppliers should hold a GFSI-recognized food safety certification such as FSSC 22000 or SQF. For consumer market access, religious certifications including Kosher (Orthodox Union or equivalent) and Halal certification (issued by accredited authorities like the Islamic Services of America - ISA) are critical. Always verify current documentation on file.
Untreated cooked sweet potato puree contains starch matrices that create high viscosity and potential retrogradation (gelation) during cold storage. Treating puree with food-grade enzymes (amylases) breaks long-chain starches into simpler sugars, reducing Bostwick viscosity, improving pumpability, and preventing syneresis (water separation) in sauces, soups, and beverages.
Yes. Custom blending solutions allow manufacturers to combine sweet potato puree with complementary ingredients—such as pumpkin, carrot, apple juice concentrate, or tropical fruit purees—to achieve specific Brix, acid, color, or flavor profiles. Co-packers can also re-pack large bulk totes or drums into customer-specified bag-in-box or pail formats with private labeling.
Quality assurance is validated through lot-specific Certificates of Analysis (COA). Standard laboratory testing includes Brix refractometry, pH measurement, Bostwick consistency testing, sensory evaluation (color/flavor), screen particle size confirmation, and comprehensive microbiological screening (TPC, Yeast & Mold, Coliforms, pathogens) under strict HACCP protocols.
Connect with our technical ingredient specialists to discuss your custom Brix targets, packaging requirements, sample requests, or custom blending needs.
Inquire Now